 DPT
Overview
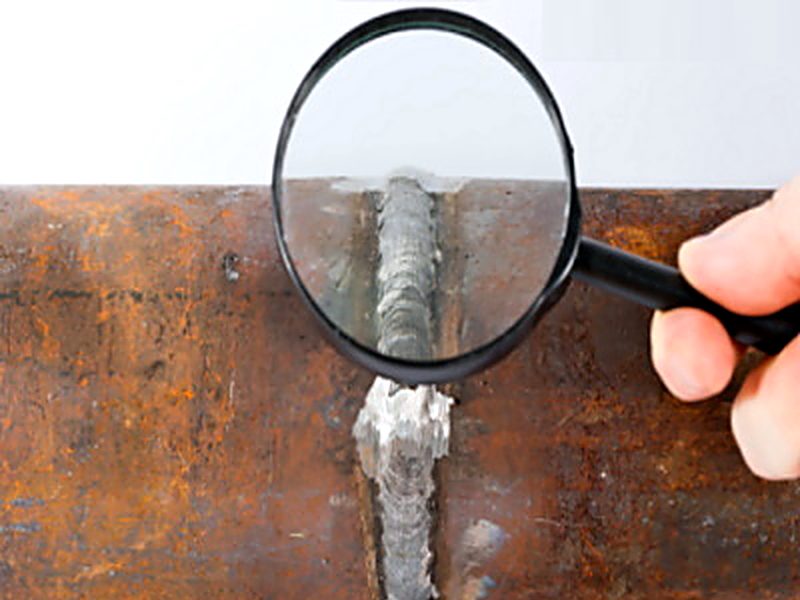
Dye penetrant testing finds cracks and defects that break the surface. A coloured or fluorescent dye is drawn into the defect, the excess is removed, and a developer draws the dye back out to show a clear indication.
It works on metals, plastics and ceramics, ferrous or not, which makes it the go-to surface method for stainless steel and non-ferrous alloys.
What it finds
- Surface cracks and crater cracks
- Porosity open to the surface
- Laps and seams
- Fatigue cracks in service
Where we use it
- Stainless steel and alloy welds
- Valve and pump components
- Machined surfaces
- Weld edge preparation checks
At a glance
| Techniques | Visible (red) and fluorescent penetrants |
|---|---|
| Typical codes | ASME Sec V Art. 6, ASTM E165, ASTM E1417 |
| Deliverables | Indication report with photographs |
Codes listed are typical. We work to the specification and acceptance criteria in your purchase order.