 Induction & furnace
Overview
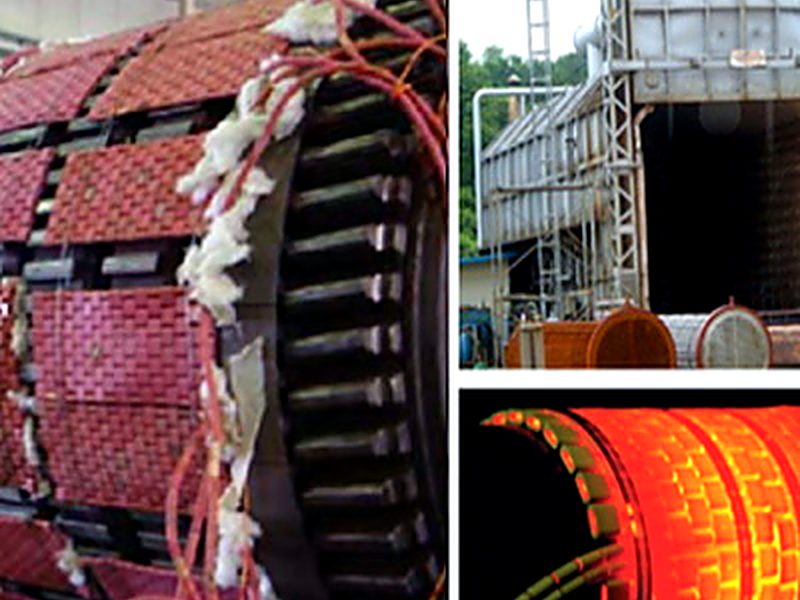
Welding and repairs leave residual stresses that can lead to cracking and distortion. We apply controlled heat to a weld repair area, a final part or an entire assembly, while protecting other areas so dimensional tolerances are not affected.
Local stress relieving is done with induction and resistance heating on site; full-component treatment is done in our furnaces. Every cycle is controlled and recorded with calibrated thermocouples and chart recorders.
What it covers
- Reduces residual welding stress
- Lowers risk of stress-corrosion cracking
- Improves dimensional stability before machining
- Restores toughness in the heat-affected zone
Where we use it
- Post-weld heat treatment (PWHT) of pipe joints
- Weld repairs on castings and valves
- Pressure vessel nozzles and shells
- Fabricated structures before final machining
At a glance
| Methods | Induction heating, resistance heating, furnace treatment |
|---|---|
| Control | Programmable controllers with thermocouple chart records |
| Typical codes | ASME Sec VIII UCS-56, ASME B31.1 / B31.3, IBR |
| Deliverables | Time-temperature charts and heat treatment certificate |
Codes listed are typical. We work to the specification and acceptance criteria in your purchase order.